White Fused Alumina #24mesh abrasive media for sandblasting TF magnets
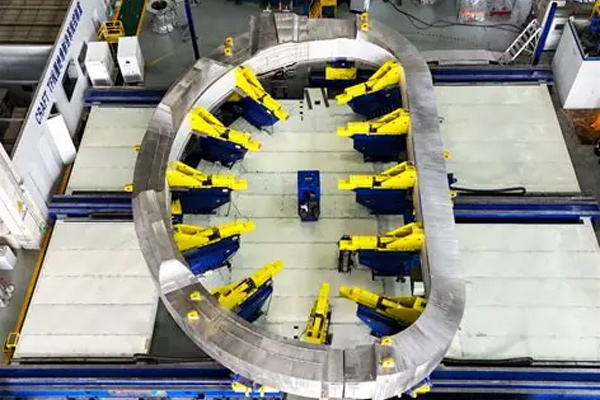
The primary substrates of TF superconducting magnets consist of 316LN/304L austenitic stainless steel, copper alloy conductors, and insulating matrices. The objectives of sandblasting are to remove surface scale and oil/grease, achieve controlled surface roughening, and enhance the bonding strength of epoxy or polyimide insulation layers. Critical constraints include the strict prohibition of ferromagnetic impurities, requirements for minimal residual contamination, controlled surface profiles, and the avoidance of introducing migratable metal ions. White fused alumina contains ≥99.2% Al₂O₃ and is virtually free of free iron and magnetism. In contrast, brown fused alumina contains iron (Fe) and titanium (Ti) impurities; under the cryogenic temperatures and strong magnetic fields characteristic of superconducting coils, these impurities can induce eddy currents, magnetic noise, and localized heating, thereby reducing critical current. Consequently, high-purity white fused alumina #24 mesh is the mandatory choice for TF magnet sandblasting, while brown fused alumina, steel grit, and iron grit are unsuitable. The specific reasons are outlined below:
Material Mechanism: White fused alumina is free of ferromagnetic impurities, meeting the stringent cleanliness requirements for superconducting magnets operating in cryogenic, high-magnetic-field environments with insulation bonding needs. Brown fused alumina and steel grit contain iron impurities, posing a risk of magnet quenching.
Particle Size Mechanism: F24 grit strikes the optimal balance between anchor pattern depth, scale removal efficiency, and substrate damage; finer grits (F46/F60) are suitable only for light roughening after precision machining and cannot effectively remove thick rolled scale.
Engineering Case Studies: For prototype TF coils in projects such as ITER, JT-60SA, and CFETR, F24 mesh white fused alumina is consistently suitable for the pretreatment of hot-rolled conductors. While WFA 46mesh is used for precision-machined conductors. Both processes are employed in parallel across domestic and international fusion engineering projects.
Risk Parameters: Due to the large particle size of F24, sandblasting pressure and post-blasting cleaning must be strictly controlled to prevent particle embedding and micro-damage to the substrate.
Regarding the deeper aspects of grit size and abrasive selection:
First, why choose 24-mesh white fused alumina?
White fused alumina 24mesh features a nominal particle size of approximately 600–850 μm. Its large, sharp-edged particles deliver high impact energy per strike, making it suitable for roughening thick oxide layers, heavy mill scale, and large-area conductor base materials; it can achieve a deep anchor profile (Rz 60–100 μm) in a single pass. Insulation bonding systems require significant anchor profile depth, and deep profiles markedly enhance the mechanical interlocking strength at the epoxy resin interface.
Finer grit sizes (F46/F60) yield only shallow profiles (Rz 20–45 μm), resulting in insufficient bonding strength; under conditions of high current and low-temperature thermal cycling, the insulation layer is prone to delamination or debonding. The baseline process for TF conductors at the domestic Institute of Plasma Physics utilizes F46—a medium-roughness option intended for conductors with lighter oxide layers—representing a distinct process route from the F24 method.
Grit sizes coarser than F24 (e.g., F12/F16) generate excessive impact energy, causing plastic deformation, surface micro-cracks, and stress concentrations in the base material. During low-temperature cycling at 4.2K, micro-crack propagation can lead to conductor fatigue failure. Furthermore, coarse grit is highly prone to particle embedment that is difficult to clean; embedded particles can act as defect sources when exposed to magnetic fields.
WFA F24 represents the optimal balance point for roughening: it provides sufficient anchor profile depth, controllable plastic deformation, and cleanability. Consequently, F24 white fused alumina is suitable for the pretreatment of conductors with thick oxide layers in the manufacturing specifications for TF coils in international fusion devices.
Second, why are other blasting abrasives not selected?
Brown Fused Alumina (BFA): Low cost but contains Fe and Ti; residual ferromagnetic impurities cause localized heating in strong magnetic fields, potentially triggering a quench, making it unsuitable for TF superconducting magnets.
Silicon Carbide (SiC): Higher hardness and strong cutting ability, but the particles are extremely brittle; upon fracturing, ultrafine powder easily embeds into the substrate and is very difficult to clean out; poses a risk of electrical conductivity, so it can’t use in insulation systems.
Steel Grit / Iron Shot: Ferromagnetic; immediately ruled out.
Glass Beads: Spherical shape; suitable only for surface finishing but unable to create a sufficient anchor profile; results in poor insulation bond strength; used only for polishing, not for surface roughening prior to bonding.